Your production line is becoming a nervous system, sensing changes and responding in real time. With Industry 4.0, you can connect IoT sensors, AI, robotics, and digital twins to improve visibility, quality, and efficiency across food manufacturing. These tools also strengthen traceability and help you anticipate equipment failures before they disrupt output. But adopting them takes more than installing new technology—it requires a coordinated shift in how you manage data, people, and production.
What Industry 4.0 Means for Food Manufacturing
Industry 4.0 connects food-processing equipment, sensors, software, and analytics into a responsive production system. For your operation, this shift means coordinating production, quality, maintenance, and planning through shared digital workflows.
Instead of managing isolated processes, you can link operational technology with enterprise systems to align recipes, schedules, inventory, and compliance records. This foundation supports supply chain integration, helping you coordinate suppliers, plants, and distribution around consistent data and changing demand.
It also enables workforce transformation: your teams can use decision-support tools, automated workflows, and digital skills to manage more complex operations. You’ll still rely on human expertise, but technology can reduce repetitive tasks and improve collaboration.
Industry 4.0 isn’t a single machine or software purchase; it’s a connected operating model that helps you adapt, standardize, and scale responsibly.
IoT Sensors Improve Production Visibility
IoT sensors give you real-time visibility into equipment performance, capturing operating data across your production line.
You can use these signals to detect anomalies early and maintain process control.
Predictive maintenance insights help you schedule service before failures disrupt production.
Real-Time Equipment Monitoring
What if production teams could spot a line slowdown before it disrupts a shift? With real-time equipment monitoring, you can track operating conditions as products move through your facility.
IoT sensors capture motor speed, vibration, temperature, pressure, and energy use, then transmit readings to dashboards your team can access immediately. Clear alerts help you identify deviations, verify equipment status, and coordinate a response before output falls behind.
You can compare live readings across lines to see where a process is changing and give operators the context to adjust controls safely.
Reliable results depend on sensor calibration, consistent connectivity, and data security that protects operational information.
Integrate monitoring with production systems, and you’ll gain a precise, shared view of equipment performance throughout each shift without relying on manual checks or delayed reports.
Predictive Maintenance Insights
When sensor data reveals a gradual rise in vibration or temperature, predictive maintenance can flag equipment at risk before it fails. You can use these insights to schedule targeted repairs during planned downtime, reducing unplanned stoppages and protecting product consistency.
IoT platforms combine readings from motors, pumps, compressors, and processing lines, then compare patterns with operating histories to detect anomalies early. Accurate sensor calibration keeps measurements reliable as conditions change, while data security safeguards production records and connected devices.
You can also link alerts to maintenance workflows, giving technicians clear priorities and equipment-specific diagnostics. By tracking failure trends across shifts, you’ll refine service intervals and spare-parts planning.
This approach turns production visibility into actionable foresight, helping your team improve uptime, control maintenance costs, and sustain safe, efficient food manufacturing.
AI Improves Food Quality and Efficiency
AI-powered vision systems inspect products in real time, helping you detect defects and maintain consistent quality.
Predictive models analyze production data to forecast demand, equipment needs, and process deviations.
With these tools, you can reduce waste and optimize throughput.
AI-Powered Quality Control
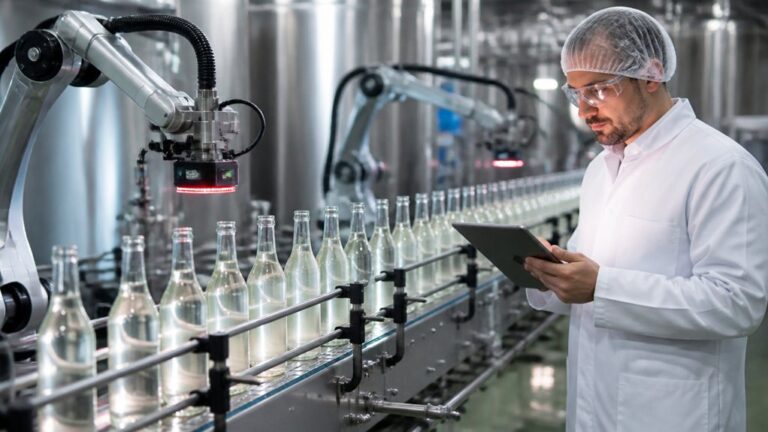
As production lines move faster and product specifications tighten, AI-powered quality control helps manufacturers detect defects in real time. With AI integration, you can combine high-resolution cameras, hyperspectral imaging, and sensor data to inspect products without slowing throughput.
Machine-learning models identify color shifts, damaged packaging, incorrect fill levels, and contamination indicators that human checks may miss. You can configure alerts to flag suspect items, trigger automated rejection, and record inspection results for traceability.
As new images and verified outcomes enter the system, models can adapt to product variations while maintaining consistent decision thresholds. This strengthens Quality assurance across each shift and reduces waste from missed defects or unnecessary rejects.
Your teams can review clear evidence, investigate exceptions, and refine inspection criteria, keeping product quality measurable, repeatable, and aligned with safety standards.
Predictive Production Optimization
Predictive production optimization uses AI to adjust process conditions before small deviations affect food quality or throughput. With predictive analytics, you can combine sensor readings, equipment histories, and product specifications to anticipate changes in temperature, moisture, or line speed.
Machine learning models identify patterns that operators might miss, then recommend precise adjustments to recipes, settings, or schedules.
You can use these forecasts to stabilize product attributes, reduce waste, and prevent unplanned downtime. For example, when a filler’s performance begins to drift, the system can flag the trend and guide you to correct it before packages fall outside target weights.
Robotics Automate Repetitive Production Tasks
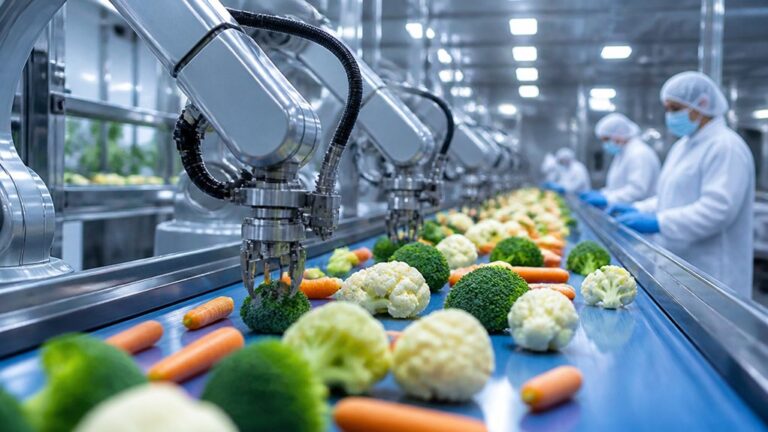
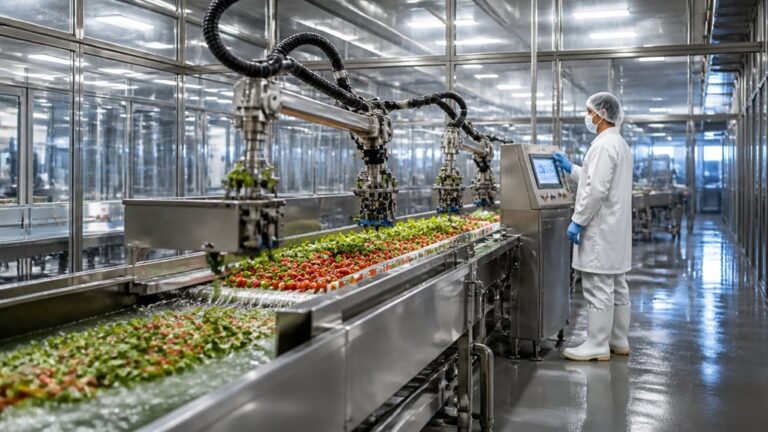
Robotics handle repetitive production tasks with consistent speed and precision, from sorting ingredients and filling containers to packaging finished products. When you automate these high-volume steps, you can maintain uniform output while reducing manual handling and repetitive strain.
Vision-guided arms identify products, adjust pick points, and reject items that don’t meet specifications. Collaborative robots work beside your staff, taking on lifting, case packing, and palletizing without isolating flexible production cells. You can reconfigure these systems for changing formats, batch sizes, and sanitation requirements.
Autonomous vehicles move ingredients and packaged goods between workstations, keeping material flowing with fewer interruptions. Sensors, safety controls, and washdown-ready components help robots operate reliably in demanding food environments.
Digital Twins Optimize Food Manufacturing
Digital twins create virtual, data-connected models of food production lines, letting you test process changes before applying them on the factory floor. By combining equipment specifications with live operating data, you can examine how line speed, temperature, mixing, or packaging adjustments affect throughput and product quality.
Virtual prototyping helps you compare equipment layouts and process configurations without interrupting production or investing in physical trials. With digital simulation, you can model bottlenecks, predict energy use, and assess responses to changing demand or ingredient properties.
These insights help you tune production parameters, reduce waste, and plan maintenance around actual equipment performance. As conditions shift, you can update the model and evaluate new scenarios quickly.
Digital twins give you a practical way to refine operations, validate decisions, and scale improvements with greater confidence.
Connected Systems Strengthen Food Safety and Traceability
When production, quality, and supply-chain systems share data, food manufacturers can trace ingredients and products across every processing stage. You can connect sensor readings, batch records, and inspection results to create a continuous, searchable product history.
If a hazard emerges, your team can identify affected lots quickly, isolate them, and target recalls instead of removing safe products unnecessarily.
Blockchain transparency can strengthen this record by making verified transactions tamper-evident across authorized partners. Integrated monitoring also flags temperature excursions, sanitation deviations, and missing documentation before they compromise product integrity.
With supplier collaboration, you can exchange consistent data on origin, certifications, and handling conditions, improving visibility from source to shipment. These connected systems support faster investigations, clearer audit trails, and more reliable compliance while helping you protect consumers and maintain trust in your products.
How to Adopt Industry 4.0 in Food Manufacturing
How can you adopt Industry 4.0 without disrupting production? Start with a focused assessment of your processes, data quality, and operational goals. Select a high-impact pilot, such as predictive maintenance on a critical packaging line, and define measurable targets for downtime, yield, and energy use.
Connect sensors and equipment through secure, interoperable platforms, then validate data flows before scaling.
Build workforce training into each phase. Give operators and technicians hands-on practice with dashboards, alerts, and digital workflows so they can act confidently and flag issues early. Establish cybersecurity controls, access permissions, and backup procedures from the outset.
Next, expand proven applications across facilities and pursue supply chain integration with suppliers and logistics partners. Use shared, standardized data to improve forecasting, inventory visibility, and quality response.
Review performance regularly, refine models, and scale investments according to verified results.
About the Author